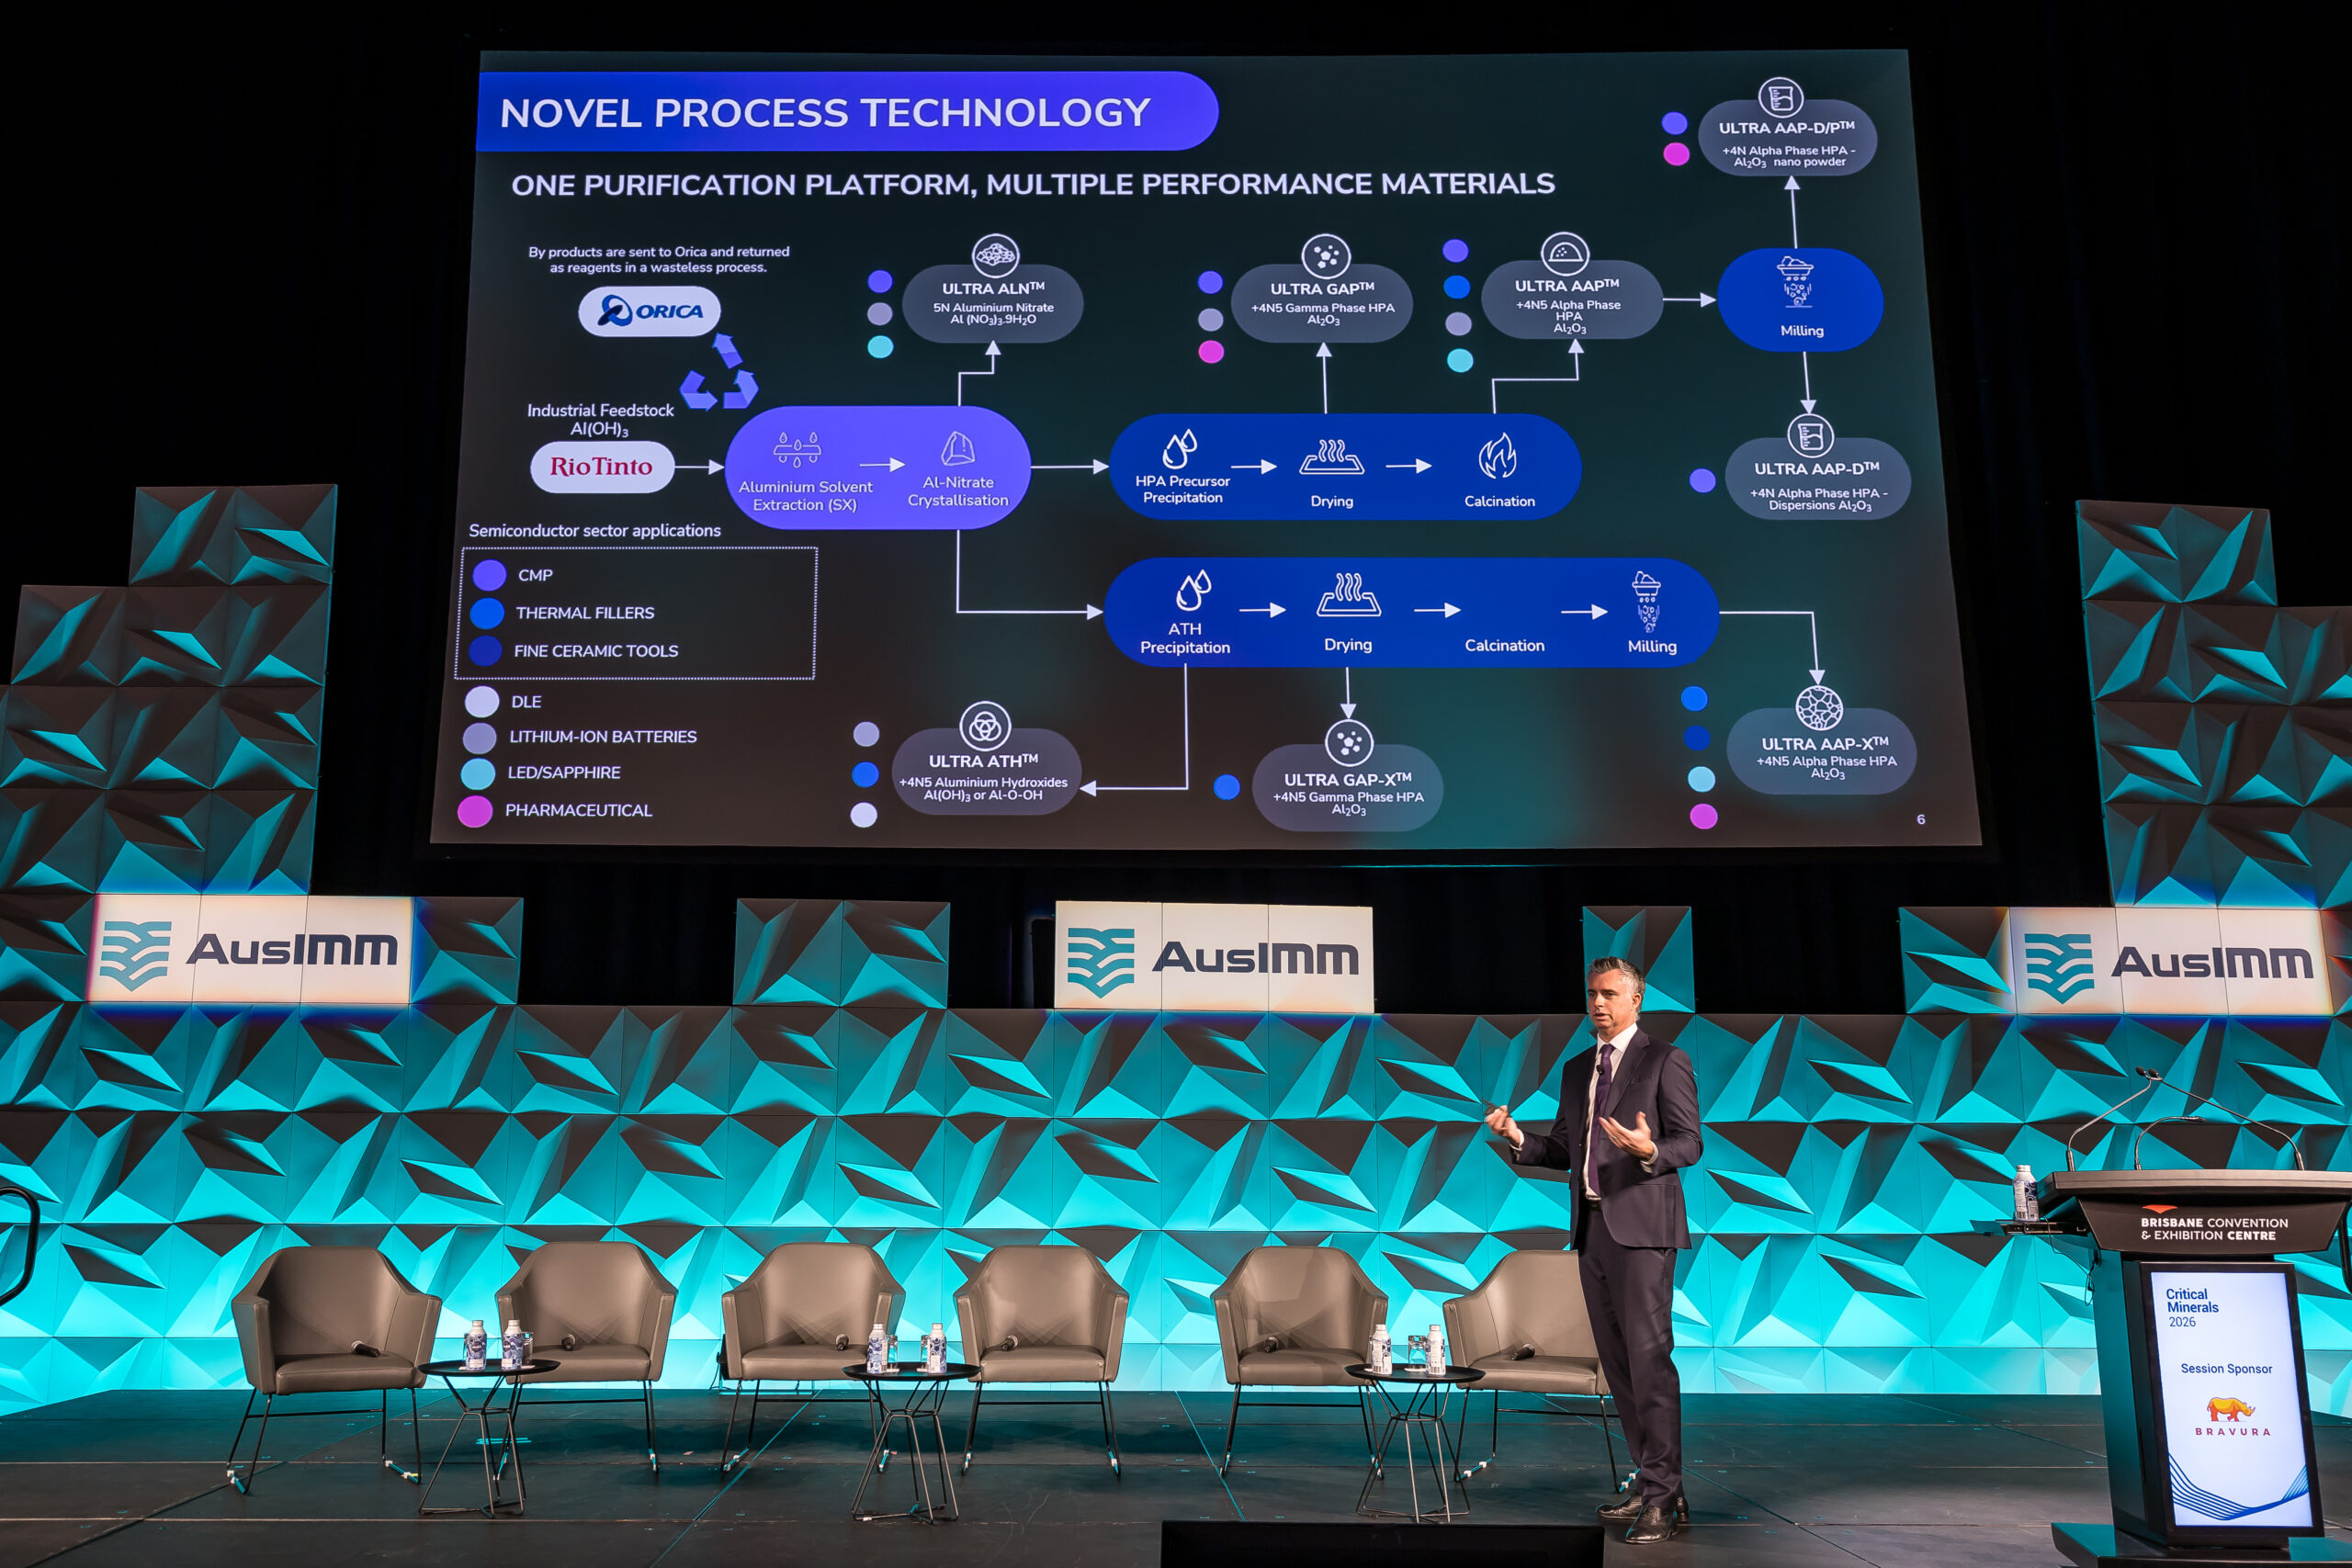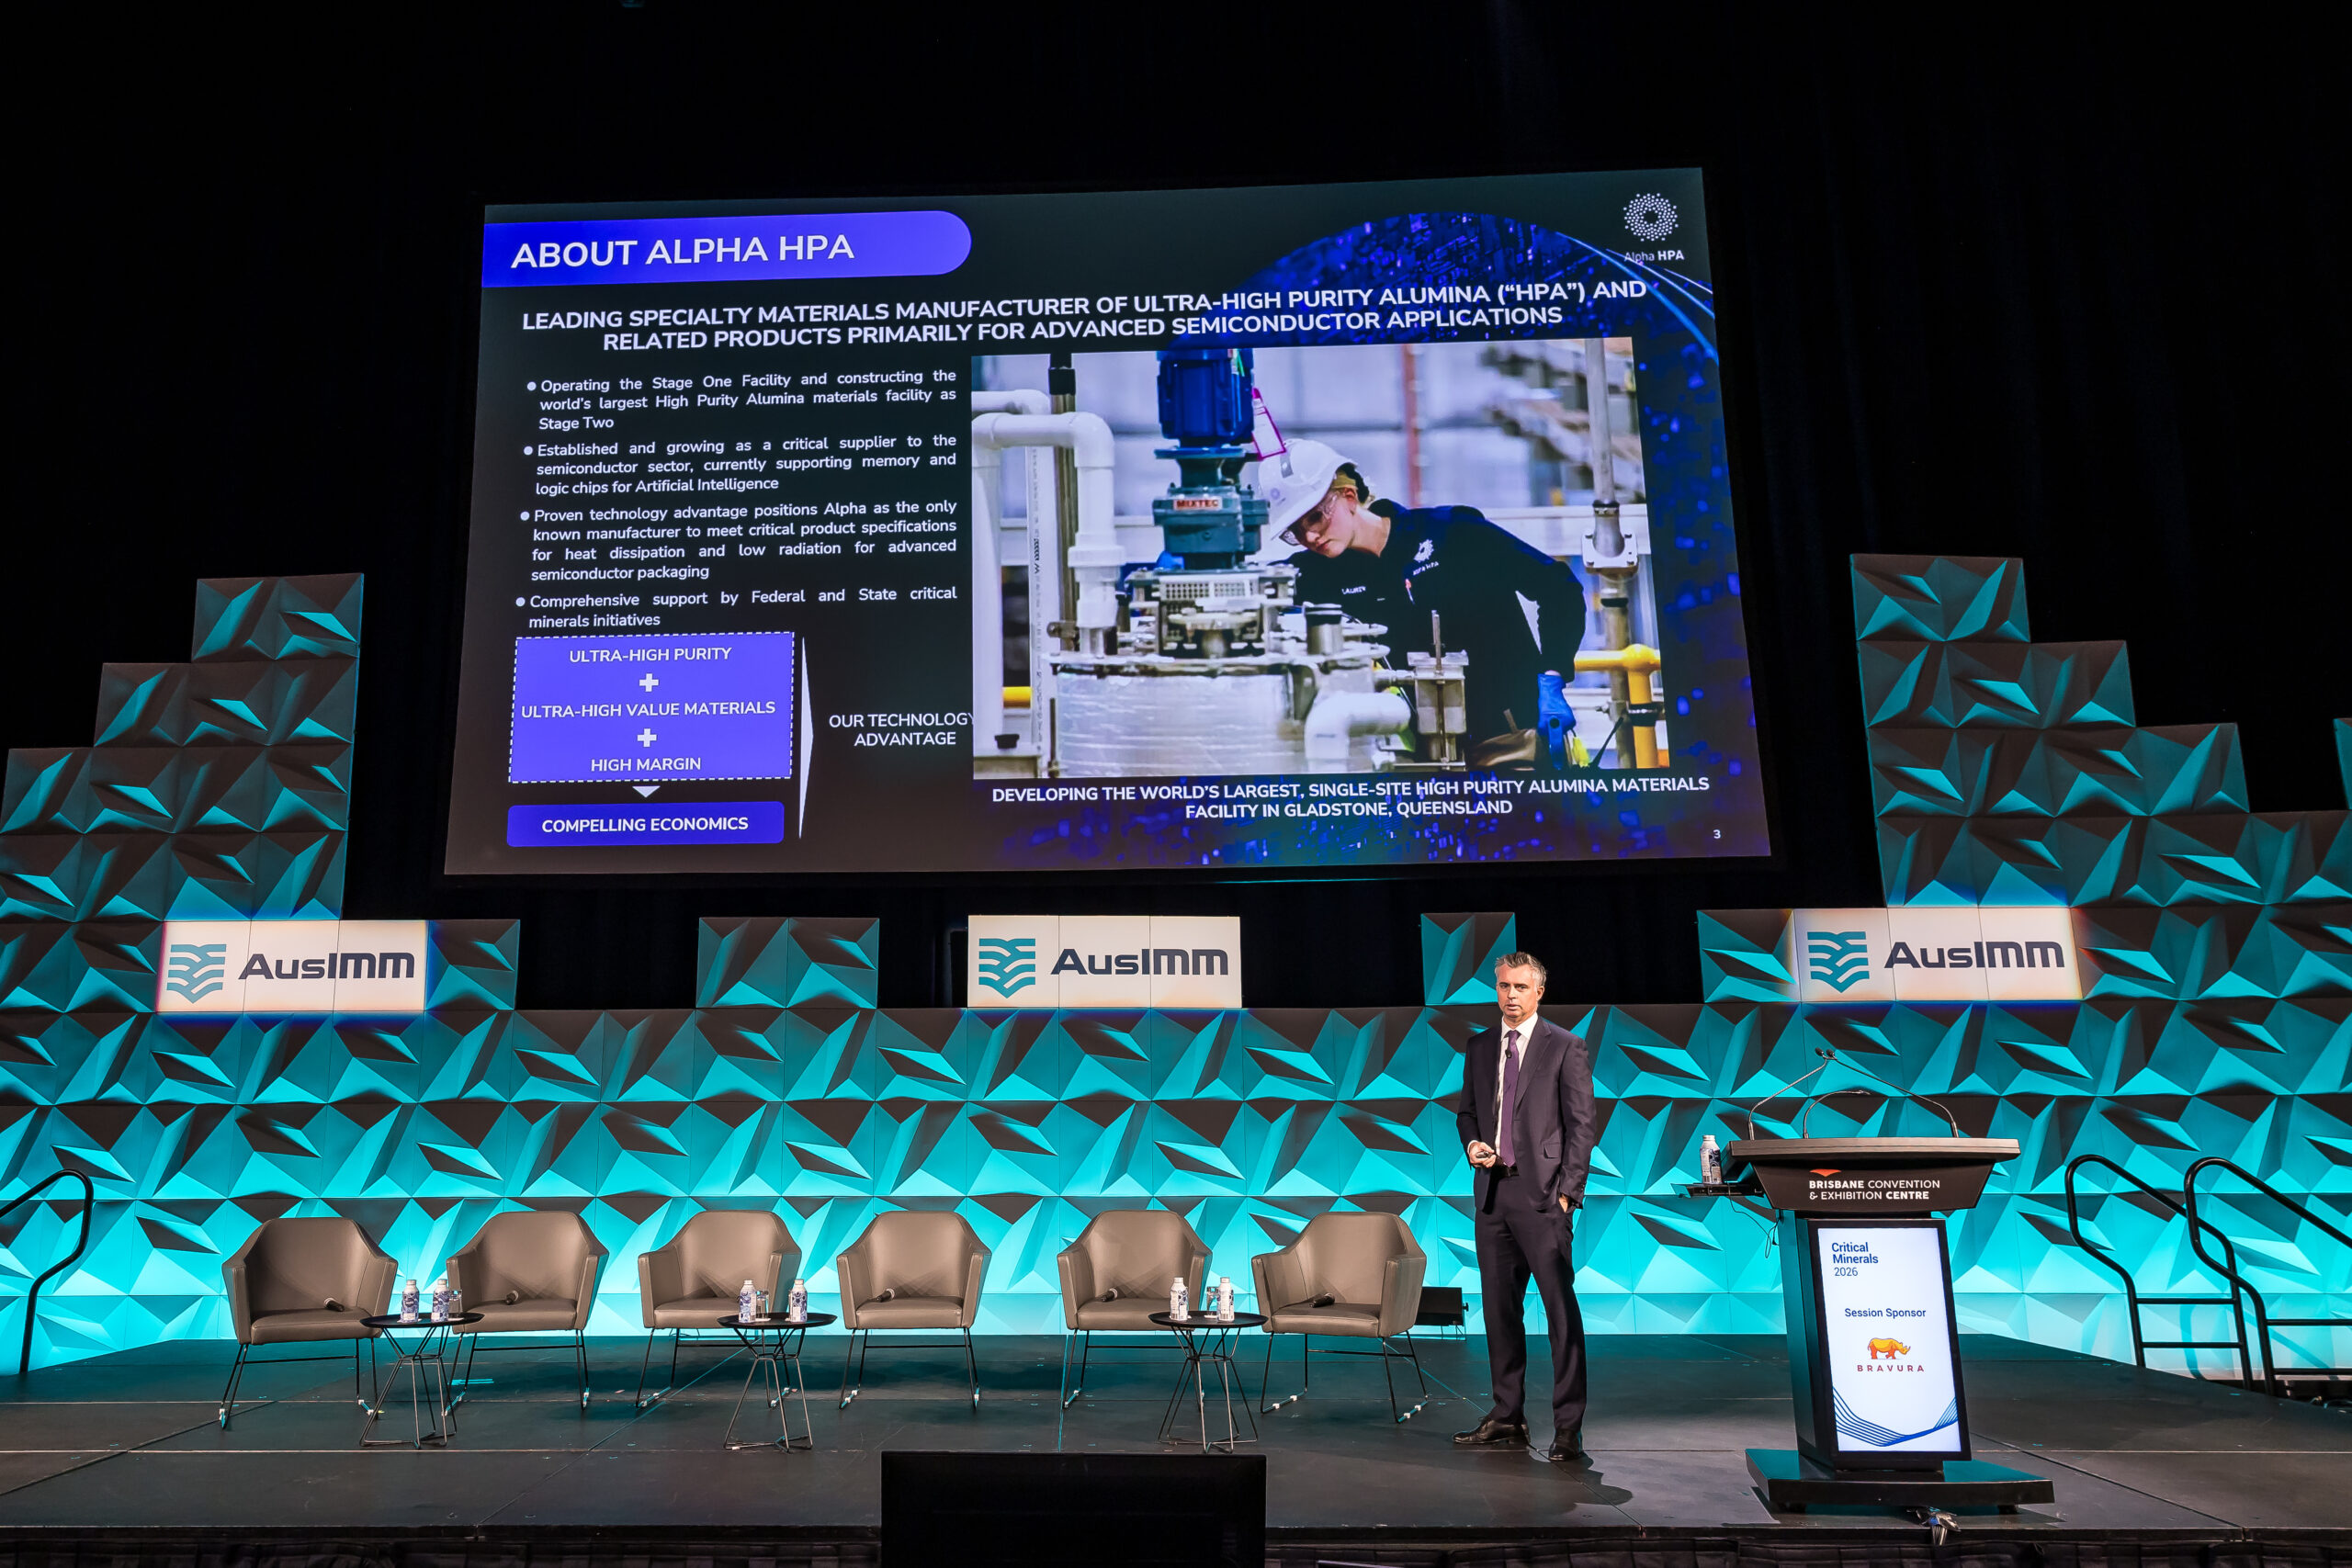
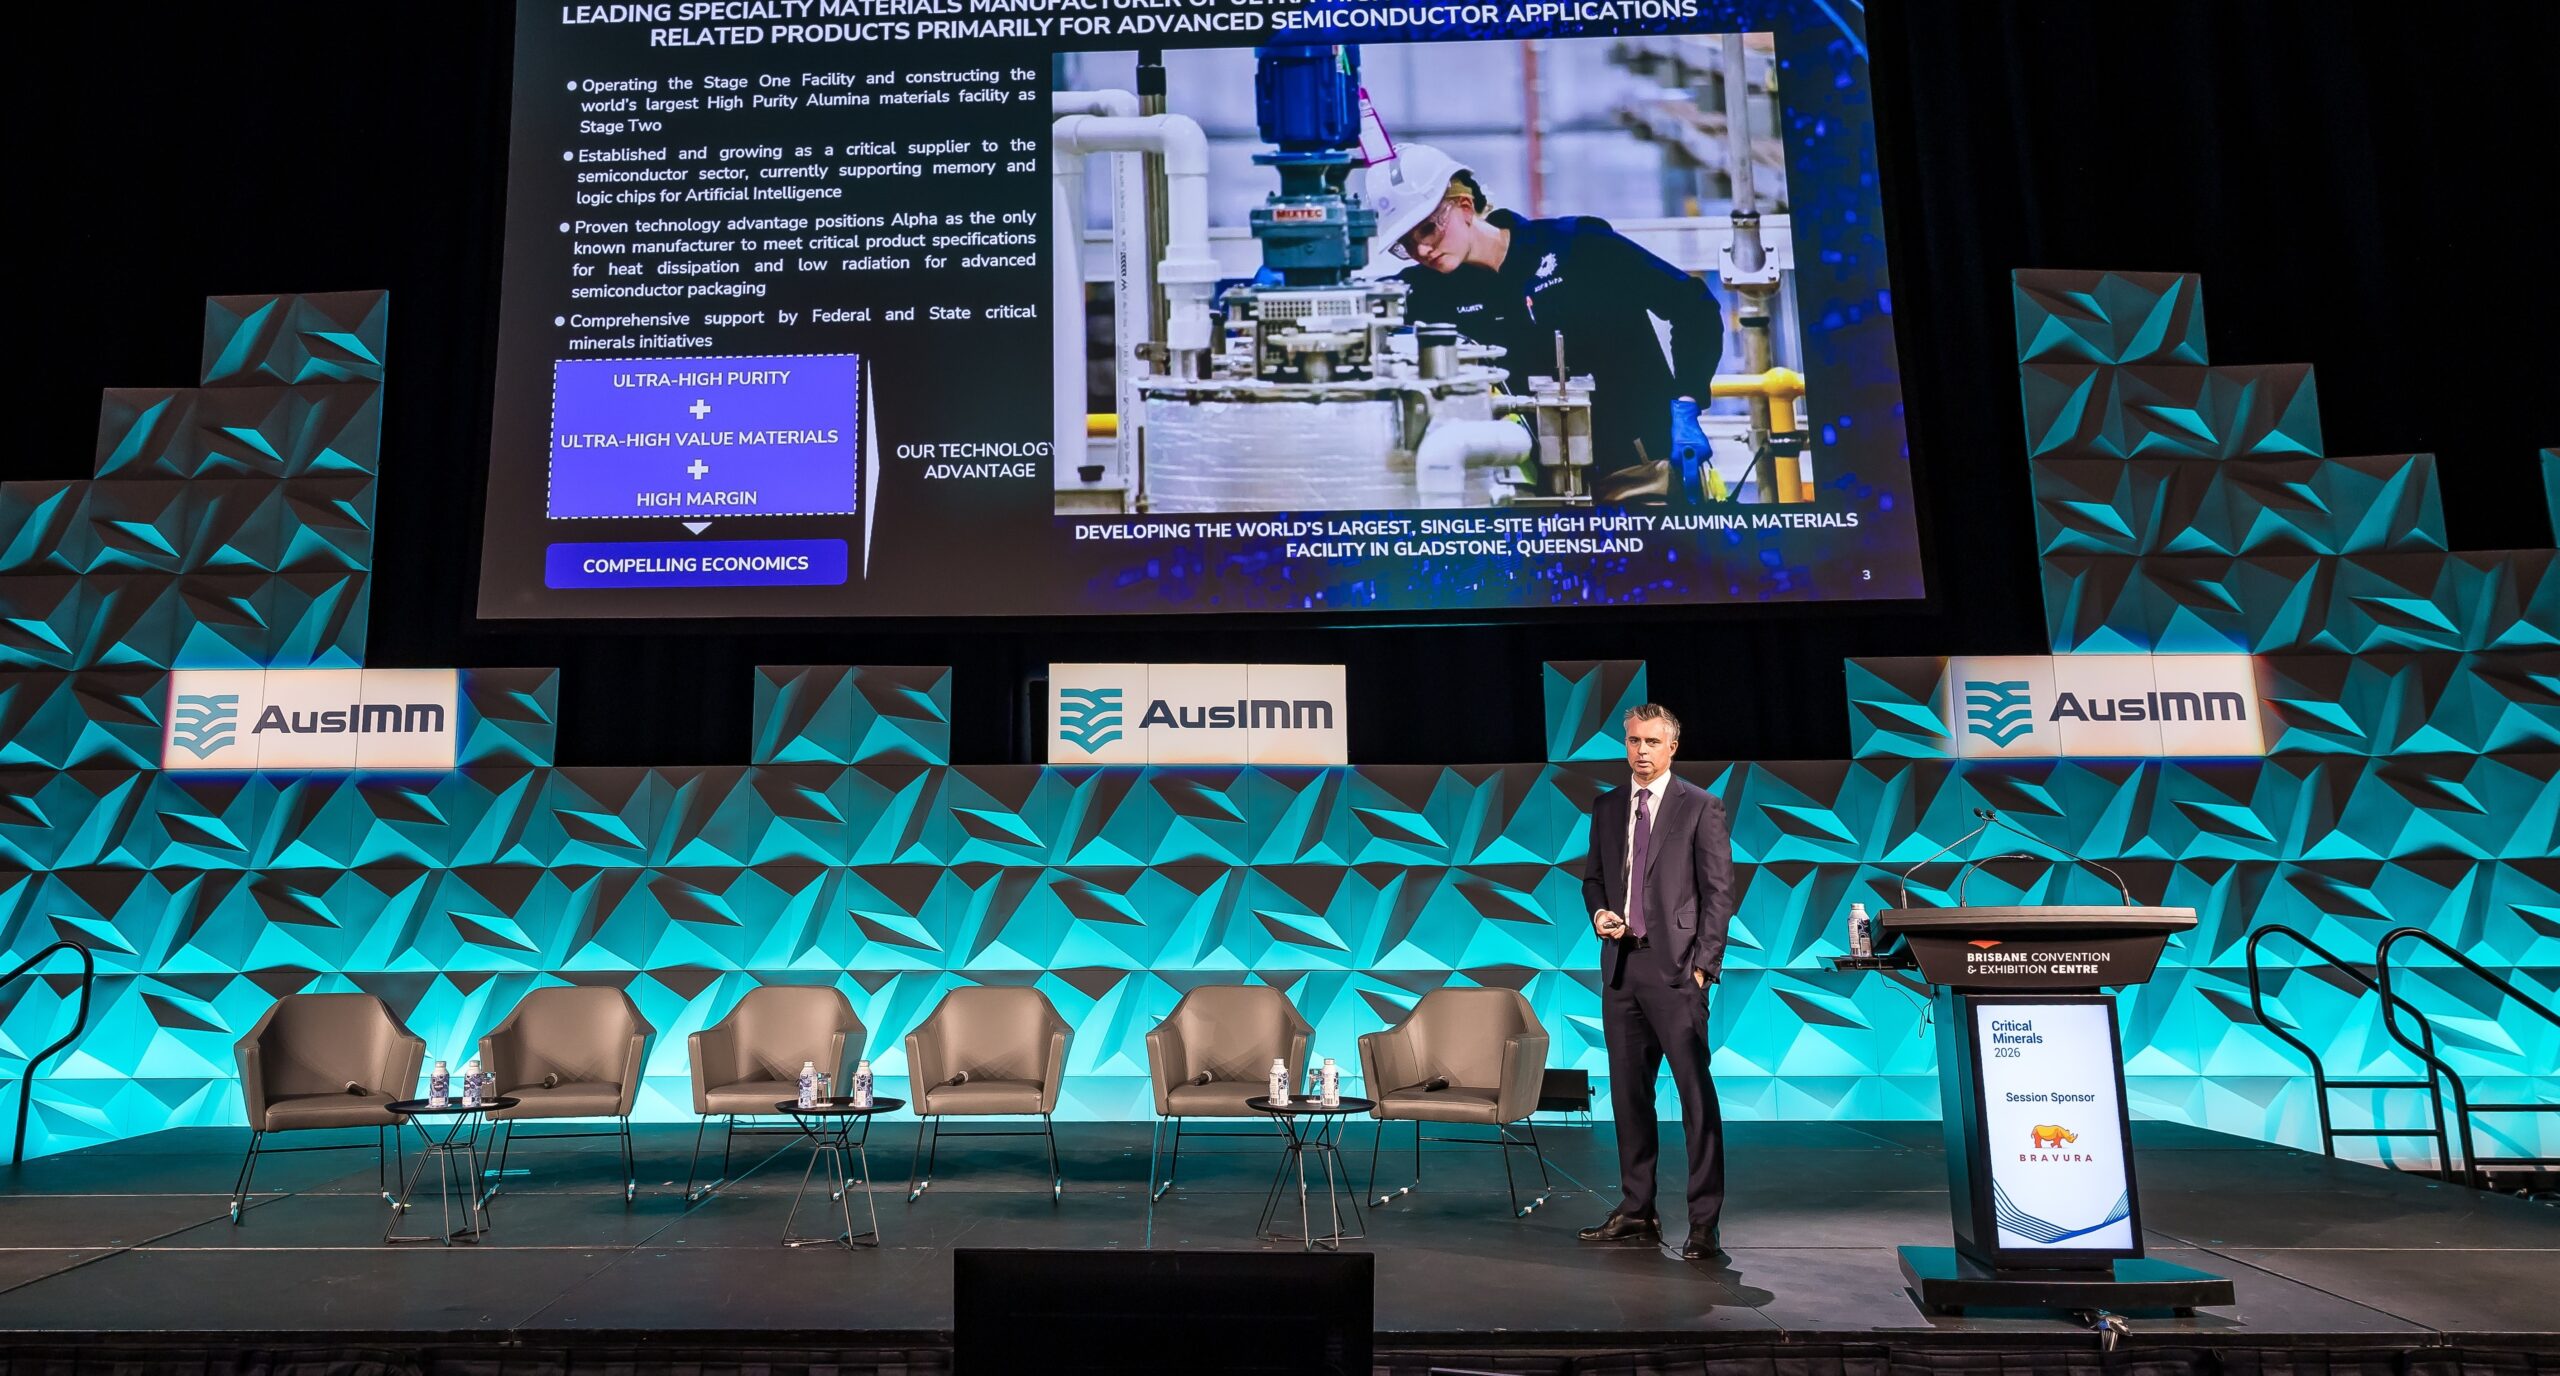
Managing Director Rob Williamson joined industry leaders at the AusIMM Critical Minerals Conference last month to share Alpha HPA's experience scaling ultra-high purity materials for semiconductor and AI applications. His presentation, Beyond the Flowsheet: Scaling Ultra-High Purity Alumina for Semiconductor and AI Infrastructure, formed part of a conference session focused on the challenge of scaling critical minerals projects from technology development to commercial production.
The presentation highlighted that developing a new process technology is only the first milestone. The greater challenge begins once the chemistry works. Alpha HPA is demonstrating what this transition looks like in practice.
For advanced semiconductor applications, success depends on consistently producing materials that meet exacting customer specifications while production volumes increase and facilities are optimised. As artificial intelligence drives growing demand across semiconductor supply chains, requirements for purity, consistency and repeatability continue to tighten.
Drawing on Alpha HPA's experience commercialising its proprietary solvent extraction technology, Rob Williamson discussed the operational realities of scaling production, including impurity control at trace levels, process stability, customer qualification and maintaining batch-to-batch consistency.
The presentation also highlighted that building globally competitive advanced manufacturing requires more than innovation alone. It takes engineering expertise, operational precision and a long-term commitment to industrial execution. It also requires developing the workforce, systems and manufacturing disciplines needed to support commercial-scale production.
The Company is currently operating its Stage One facility while progressing construction of the HPA First Facility Stage Two expansion in Gladstone. Together, these facilities are designed to support the manufacture of ultra-high purity alumina and related products for advanced technology markets, particularly semiconductor applications.
Product demand continues to validate the opportunity, with aggregated end-user Letter of Intent volumes now reaching 13,780 tonnes per annum and FY27 demand for Alpha HPA’s materials effectively rendering the Stage One facility approximately four times oversubscribed. Having demonstrated the technology and established commercial demand, the focus now is on expanding that capability and delivering qualification-ready products consistently at larger scale.